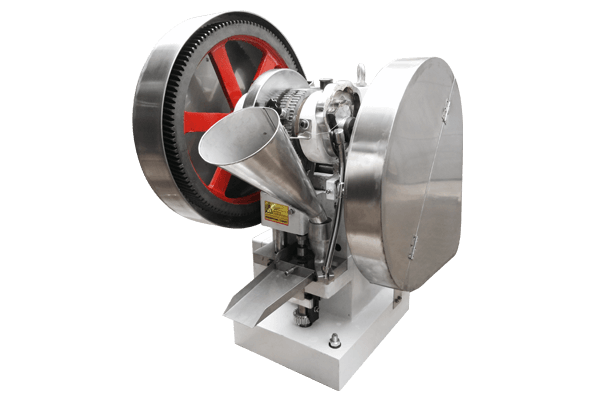
A single punch tablet press uses one compression station with an upper punch, lower punch and die. It is commonly considered for formulation trials, samples and small batches where the operator needs to observe filling, compression and ejection before moving to a higher-output press. It is not automatically the right choice for every powder or production target.
What Is a Single Punch Tablet Press?
A single punch press is a tablet compression machine with one working station. Powder or granules enter a die cavity, the upper and lower punches apply compression, and the formed tablet is ejected. The term “single punch” can be misleading: the machine normally uses a matched upper punch, lower punch and die rather than one punch acting alone.
This layout is easier to observe than a multi-station rotary press. That can be useful during product development, training or small-batch work, especially when the tablet dimensions and powder behavior are still being confirmed. It does not remove the need for a suitable formulation, tooling and quality controls.
How the Compression Cycle Works
1. Die filling
Prepared powder or granules move from the hopper or feed arrangement into the die cavity. Consistent filling depends on flow behavior, particle-size distribution, moisture condition and the way material reaches the die. A press cannot compensate for every feeding or segregation problem.
2. Fill adjustment
The lower punch position defines the available die volume on many single-station machines. This setting influences tablet weight, but weight consistency must be checked through an appropriate sampling and control procedure. Changing fill depth alone does not ensure uniform active-ingredient content.
3. Compression
The upper punch enters the die while the lower punch supports the powder bed. Applied force, tablet geometry, tooling condition and formulation behavior influence the resulting tablet. Hardness, thickness and appearance should be evaluated together rather than treating one machine setting as a universal answer.
4. Ejection and discharge
After compression, the upper punch withdraws and the lower punch raises the tablet for removal or discharge. Excessive ejection resistance, sticking or visible damage can indicate a tooling, lubrication, moisture, formulation or operating issue that requires investigation.
When a Single Punch Press Is a Practical Fit
A single-station machine may be appropriate when the main objective is controlled small-batch work rather than continuous high output. Typical discussions include:
- formulation trials and early tablet-development work;
- samples for dimensional, appearance or packaging checks;
- teaching and process-demonstration tasks;
- small batches with planned cleaning between products;
- projects that need closer observation of each compression cycle.
Suitability still depends on the material and quality requirements. Pharmaceutical, supplement, food and industrial tablets can involve different documentation, cleaning and product-contact expectations. The buyer should define the application instead of assuming that one machine configuration fits every industry.
When to Consider a Multiple Punch or Rotary Press
A single punch press is usually a poor fit when hourly output is the primary requirement, when the process must run continuously, or when material handling and downstream equipment need to be integrated into a production line. Once the formulation, tooling and in-process controls are established, a multi-station machine may provide a more appropriate production workflow.
| Selection point | Single punch direction | Multiple punch or rotary direction |
|---|---|---|
| Primary purpose | Trials, samples or smaller batches | Repeated production and higher throughput |
| Process observation | One station is easier to observe directly | Several stations require broader process control |
| Changeover | Useful where product changes are planned and controlled | Better when a stable product justifies a production setup |
| Buying priority | Tablet feasibility and operating fit | Output, feeding, tooling system and line integration |
Buyers can compare the wider machine categories on the tablet press selection page or review the current multiple punch tablet press direction.
Information That Should Be Confirmed Before Selection
Tablet dimensions and tooling
Provide the target diameter, thickness, shape and any embossing requirement. A drawing or a physical sample is more useful than a product name alone. The punch and die set must match the tablet design and the selected press.
Powder or granule behavior
State whether the material is free-flowing, cohesive, moisture-sensitive, abrasive or known to stick. If the formulation is still under development, make that clear. Equipment selection and formulation development are related, but they are not the same task.
Batch purpose and operating schedule
Define whether the press will be used for occasional trials, daily small batches, training or routine production. Include the intended batch quantity and the number of product changes. These details affect the choice between a single-station press and a higher-output system.
Site and documentation requirements
Confirm electrical supply, installation space, destination country, cleaning procedure and required documentation. For regulated products, identify the applicable quality system and validation responsibilities before ordering equipment.
Quality Checks the Machine Cannot Replace
A tablet press forms the tablet, but it does not by itself prove blend uniformity, content uniformity, strength, dissolution performance or shelf life. Those requirements depend on the product, formulation, validated process, sampling plan and applicable regulations.
For drug products, FDA current good manufacturing practice requires scientifically sound specifications and adequate process controls. FDA also identifies blend and content uniformity as important for limiting dose-to-dose variation. Equipment claims should therefore remain separate from product-quality evidence. See the FDA overview of current good manufacturing practice.
Common Compression Problems: What to Investigate
Observed defects should be investigated systematically rather than corrected with a generic recipe.
| Observed issue | Areas to review |
|---|---|
| Tablet weight variation | Material flow, segregation, die filling, fill setting and sampling method |
| Sticking or picking | Moisture, formulation, punch-face condition, tooling cleanliness and operating conditions |
| Capping or lamination | Entrapped air, formulation, granule condition, compression profile and ejection |
| Chipping or difficult ejection | Tooling condition, tablet design, lubrication, formulation and die-wall friction |
| Inconsistent hardness or thickness | Fill consistency, compression setting, tooling wear and material variation |
Changing pressure or adding an excipient without supporting formulation work may hide one symptom while creating another. Record the condition, isolate variables and use qualified formulation and quality personnel where the product requires them.
Cleaning and Maintenance Questions for Buyers
Before purchase, ask how the hopper, feed path, punch and die area can be accessed and cleaned. Confirm the stated materials for product-contact parts and how tooling is removed. Maintenance planning should cover inspection of punches and dies, fasteners, guards, drive components and lubrication points according to the equipment manual.
Lubricants used for mechanical components must be managed so they do not contaminate product-contact areas. Cleaning and maintenance records are also important where products or formulations change between batches.
Single Punch Tablet Press RFQ Checklist
Send the following information when requesting a model check:
- product type and whether the material is powder or granules;
- target tablet diameter, thickness, shape and drawing or sample photo;
- intended batch quantity and operating frequency;
- known flow, sticking, capping or ejection concerns;
- required tooling and whether embossing is needed;
- available voltage and frequency;
- installation country and site constraints;
- cleaning, documentation or qualification requirements.
Lanphan’s single punch tablet press page provides the current product-selection route. A useful quotation should identify the proposed equipment and included tooling rather than relying on a general capacity statement.
Frequently Asked Questions
Can a single punch press make every tablet shape?
No. Feasibility depends on the tooling system, tablet dimensions, shape, embossing and material behavior. Send a drawing or sample for review.
Will a single punch press solve poor powder flow?
Not necessarily. Flow, segregation and die filling must be considered before compression. The correct response may involve formulation, granulation, feeding or equipment changes.
Is a single punch press suitable for production?
It may suit defined small-batch work, but it should not be selected for a production target without comparing output, changeover, feeding and quality-control requirements with a multi-station press.
What should be tested before scaling up?
Confirm that the formulation, tablet dimensions, tooling and quality criteria are stable enough for a production workflow. Scale-up decisions should use documented process and product data rather than a successful visual sample alone.
 English
 Russian
 Arabic
 Spanish